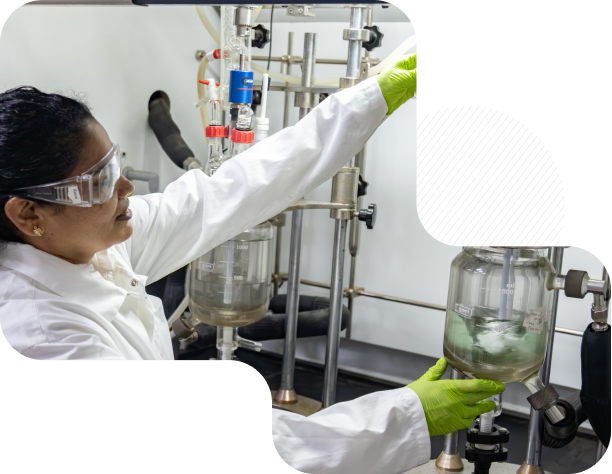
Aarti Pharmalabs Limited (APL) has transformed from a vendor to a preferred partner. Our two cutting-edge R&D facilities, located across Maharashtra and Gujarat, consistently strive for:
 Route Scouting and Design
New Product Development
Process Optimization and Scale-up
Life Cycle Technology Management
APL has developed expertise in various chemistries and to name a few:
Expertise in developing stereoselective synthetic routes to generate chiral molecules with high enantioselectivity and diastereoselectivity, supporting the efficient development of complex pharmaceutical compounds.
Application of biocatalytic and chemocatalytic approaches to develop selective, efficient, and sustainable synthetic processes. Our capabilities include catalyst/enzyme screening, reaction optimization, and process development for challenging transformations like enantioselective transformations, chiral resolution, and selective functional-group modifications
One of India’s Largest Hydrogenation Facilities. Proven expertise in hydrogenation chemistry, including catalytic hydrogenation, Fixed bed Hydrogenation, Loop Hydrogenation and selective reduction of diverse functional groups. We optimize catalyst, solvent, pressure, and reaction conditions to achieve high conversion, selectivity, and process robustness.
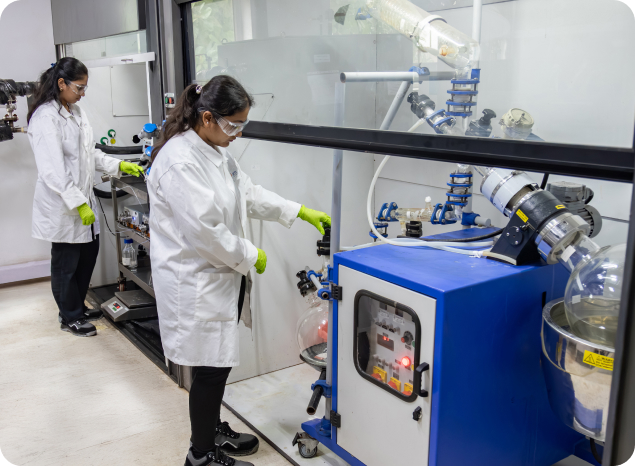
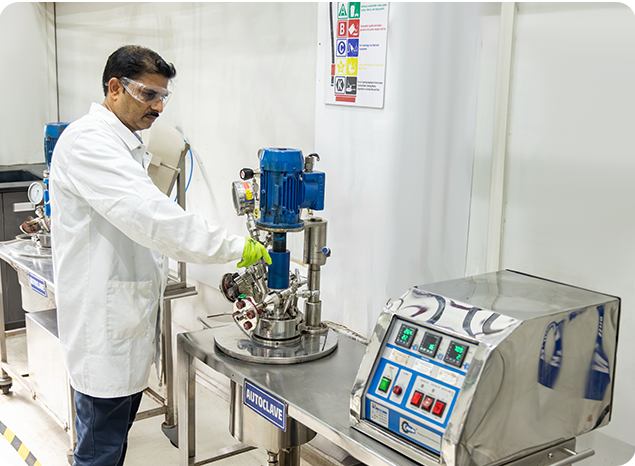
Experience with organometallic and metal-mediated transformations, including Grignard, organolithium, and transition-metal-catalyzed reactions. Our expertise supports challenging bond-forming transformations and scalable process development.
Capability to safely develop and scale reactions requiring controlled low-temperature conditions (up to -1000C). Our expertise covers reaction optimization, heat-transfer considerations, reagent addition strategies, and safe handling of highly reactive intermediates.
Cyanation is one of our key process chemistry capabilities, backed by extensive experience in the safe and efficient execution of cyanide-based transformations at large scale. One of our manufacturing facilities is equipped to handle sodium cyanide (NaCN) consumption of 1–2 MT per day, supported by robust process controls and dedicated safety systems.
Innovation is at the core of our R&D strategy. We continuously evaluate next-generation chemistry platforms to develop more efficient, sustainable, and scalable solutions for complex pharmaceutical molecules. Our current areas of exploration include:
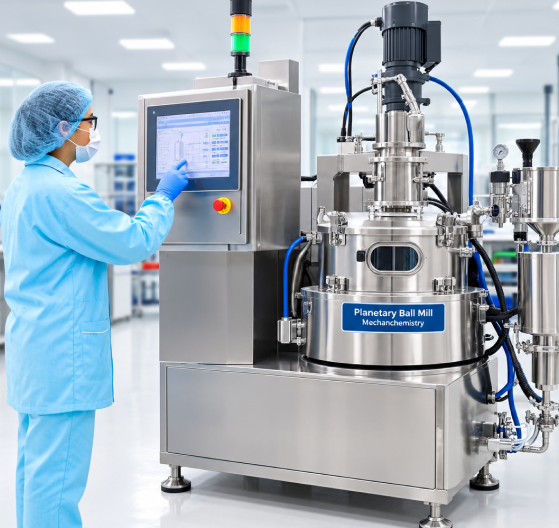
Exploring solvent-minimized and mechanically driven reactions to enhance process efficiency and sustainability.
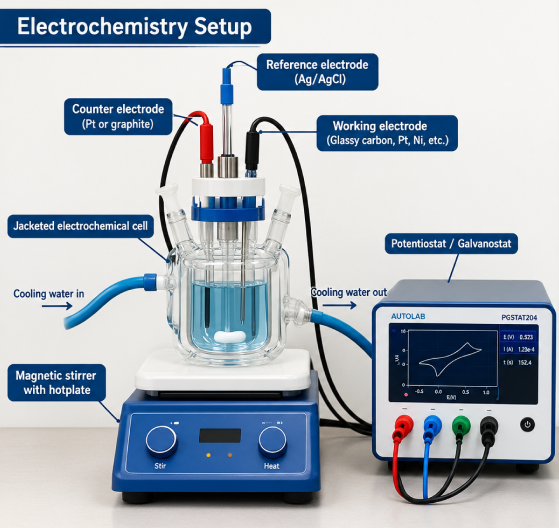
Investigating electrochemical transformations as alternatives to conventional oxidation and reduction methods, with potential benefits in selectivity, safety, and process efficiency.
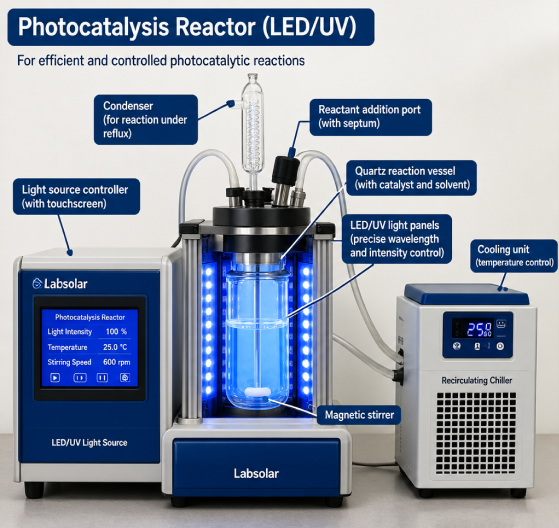
Exploring light-driven chemical transformations to enable novel reaction pathways and efficient synthesis of complex molecules.
Exploring solvent-minimized and mechanically driven reactions to enhance process efficiency and sustainability.
Investigating electrochemical transformations as alternatives to conventional oxidation and reduction methods, with potential benefits in selectivity, safety, and process efficiency.
Exploring light-driven chemical transformations to enable novel reaction pathways and efficient synthesis of complex molecules.
Our R&D teams are actively exploring these technologies for future applications in pharmaceutical process development and manufacturing.
To learn more, reach out at:
cdmo@aartipharmalabs.com
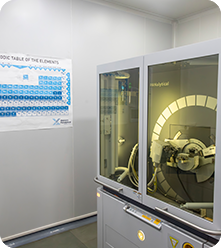
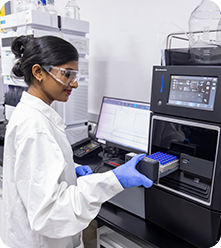
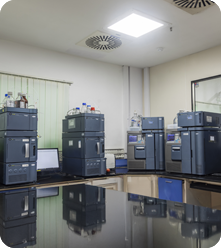
Our R&D labs are designed to accelerate innovation and transform complex challenges into scalable solutions. With 200+ process and analytical scientists, advanced equipment, and specialized capabilities, we offer comprehensive expertise across process development, analytical development, optimization, and scale-up.
From early-stage development to commercial readiness, our integrated R&D capabilities enable faster development, robust processes, and reliable scale-up for simple to complex drug substances.