Aarti Pharmalabs Limited (APL) is a leading small-molecule CDMO in India, providing Contract Development and Manufacturing Services (CMC Services) for drug substances, including NCEs, HPAPIs, RSMs and intermediates. We partner with global innovator pharmaceutical and biotechnology companies across the complete development lifecycle- from laboratory and pilot scale through clinical development, launch and commercial manufacturing.
Our value proposition is built around strong scientific excellence, speed, flexibility and partnership. Dedicated scientific and project teams work closely with clients to accelerate development, enable efficient scale-up and deliver reliable manufacturing solutions. We operate as an extension of our clients’ laboratories and teams, providing the expertise and capabilities needed to move molecules from development to commercial success.
At APL, we aspire to be the preferred CDMO partner for our clients – helping them bring innovative medicines to patients faster. We recognise the trust our clients place in us with their development programmes and are committed to earning that trust through technical excellence, responsiveness, quality and a strong culture of partnership.


Our process development chemists provide route scouting, process development, and process optimization services based on Design of Experiments (DoE) and Quality by Design (QbD) principles. We deliver APIs, key intermediates, and regulatory starting materials from gram to kilogram scale, supporting development milestones from early clinical stages through commercial manufacturing.
Explore new synthetic routes or redesign and optimize existing routes to reduce cost, improve quality, enhance process safety, and enable robust scalability.
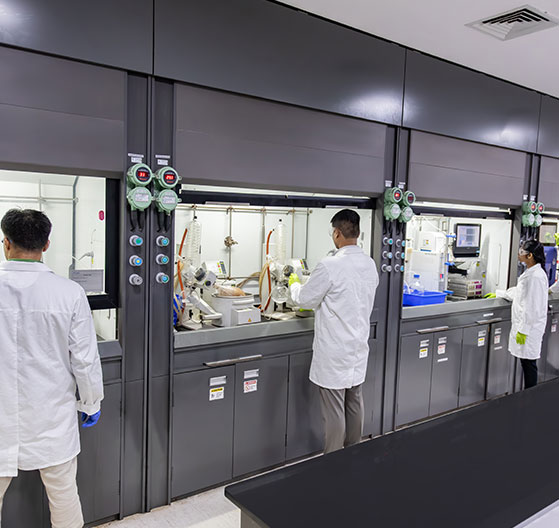
Rapidly develop and optimize critical reaction steps using DoE and QbD principles, where appropriate.
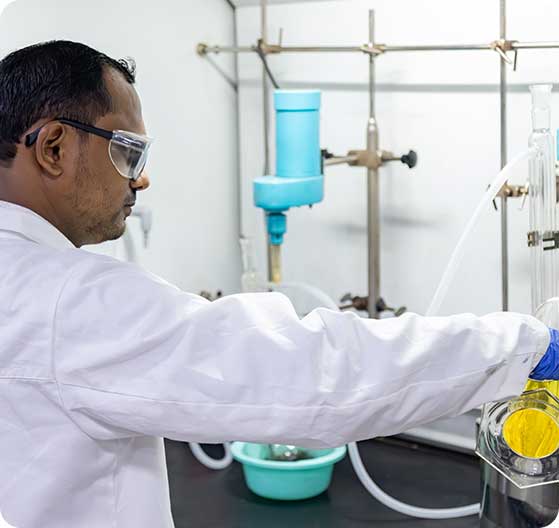
Address challenging chemical transformations using technologies such as flow chemistry, photochemistry, enzymatic chemistry, and other advanced process technologies.
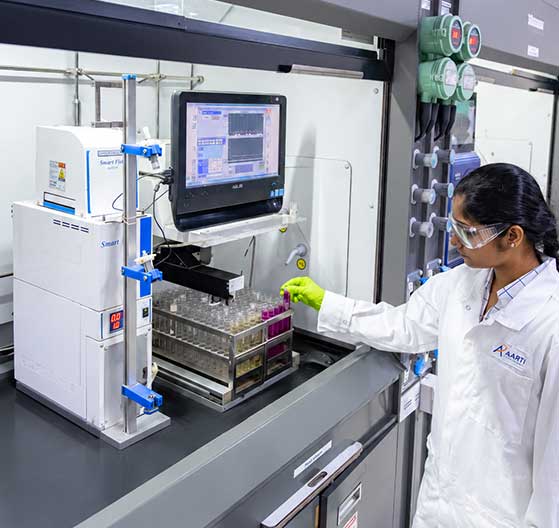
Through systematic experimentation and process understanding, our scientists identify the Critical Quality Attributes (CQAs) of an API and the Critical Process Parameters (CPPs) that influence them. This enables us to establish a robust design space with built-in flexibility, supporting consistent quality, accuracy, and reproducibility during scale-up and technology transfer to manufacturing.
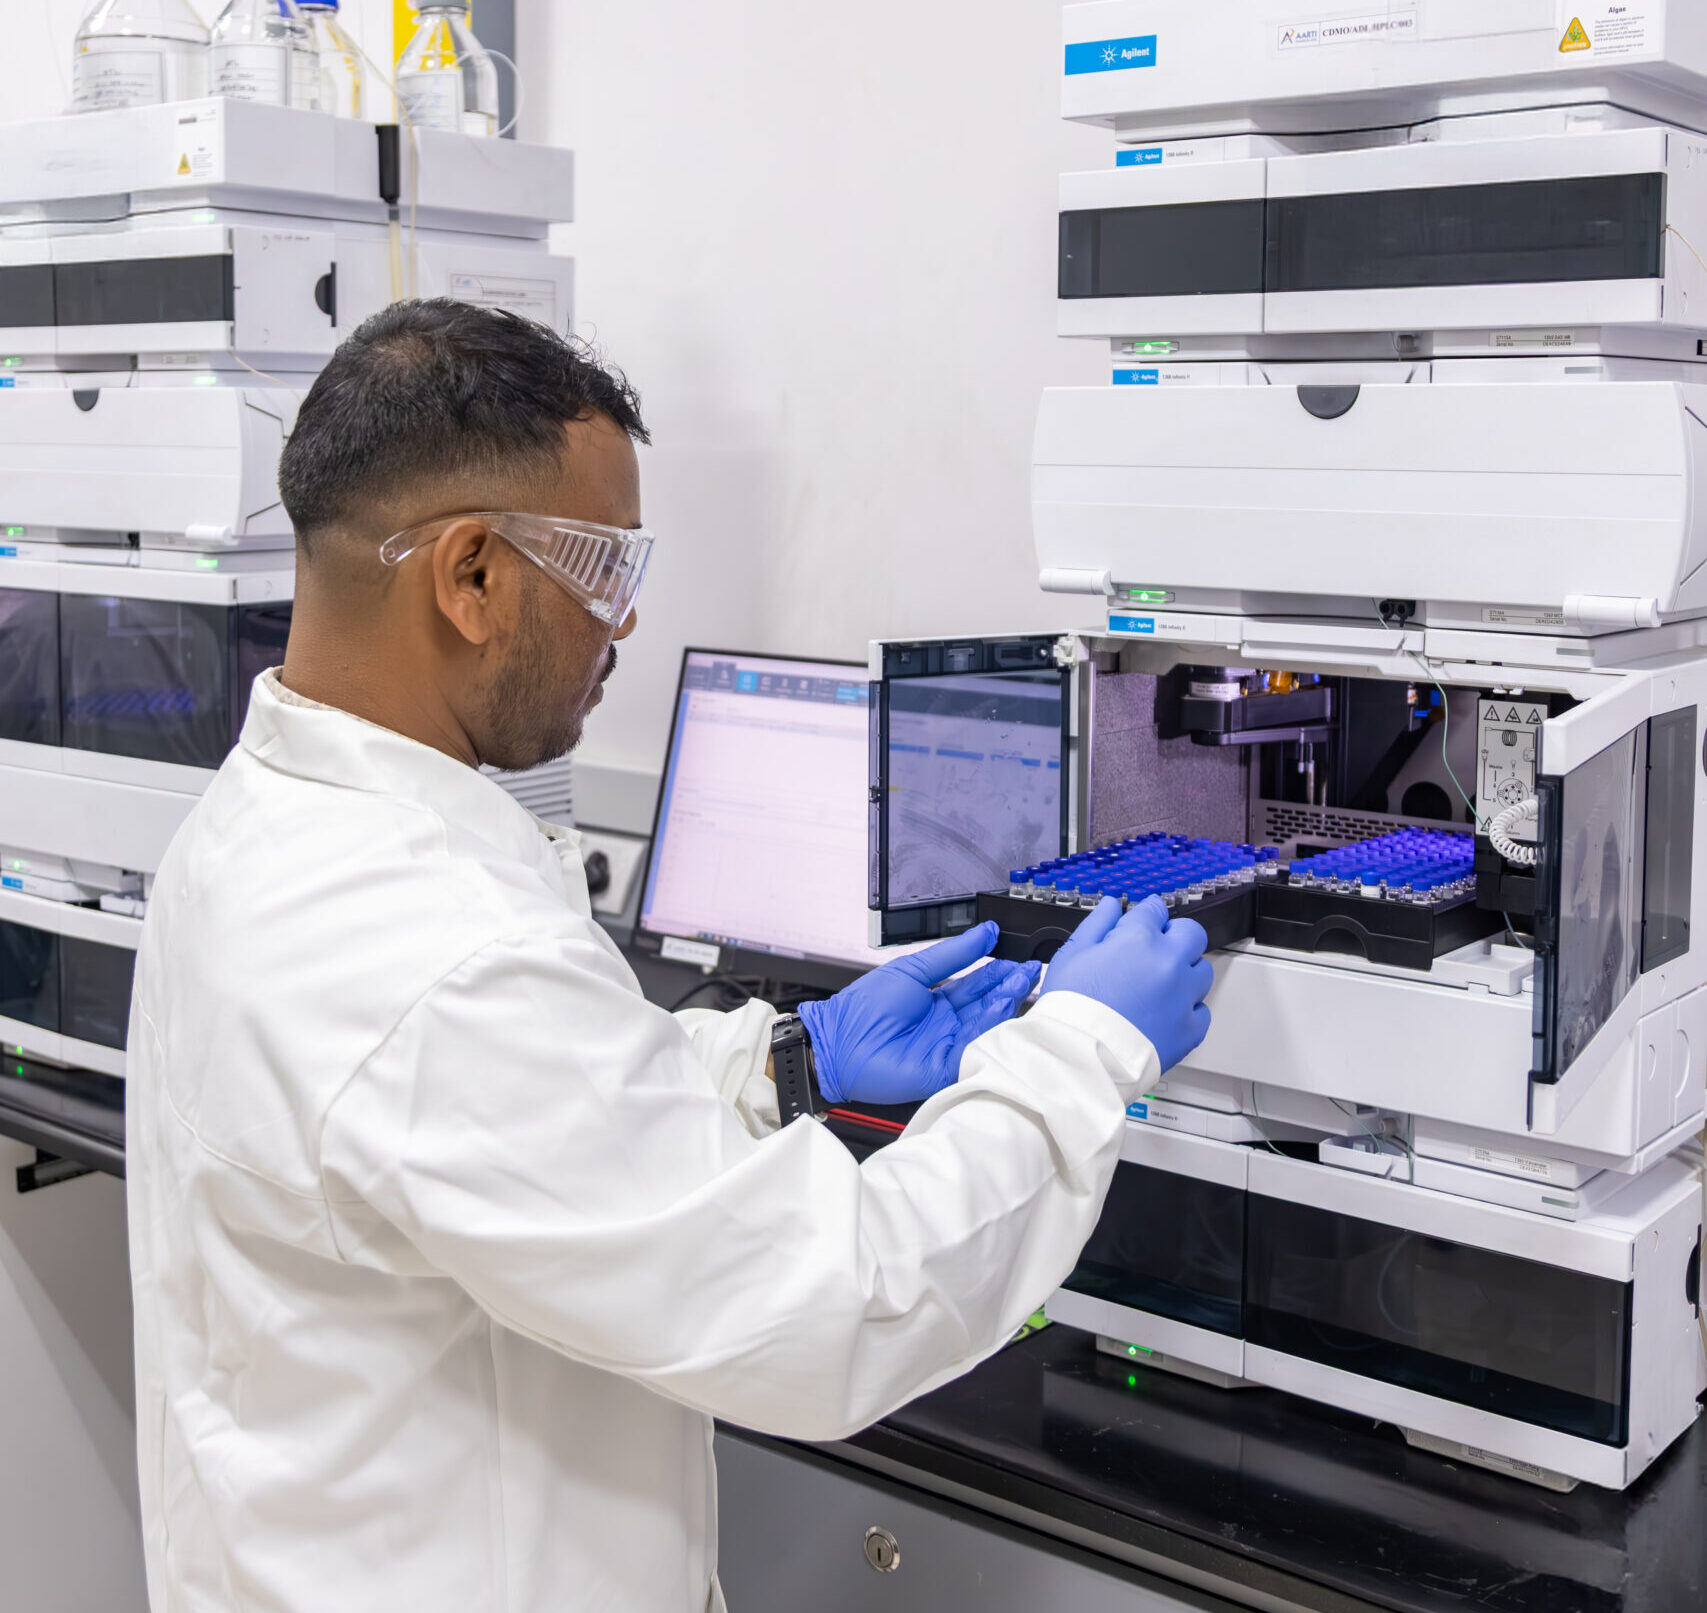
Synthesize, isolate, and characterize impurities; investigate their potential mechanisms of formation; and develop effective impurity purging and control strategies.
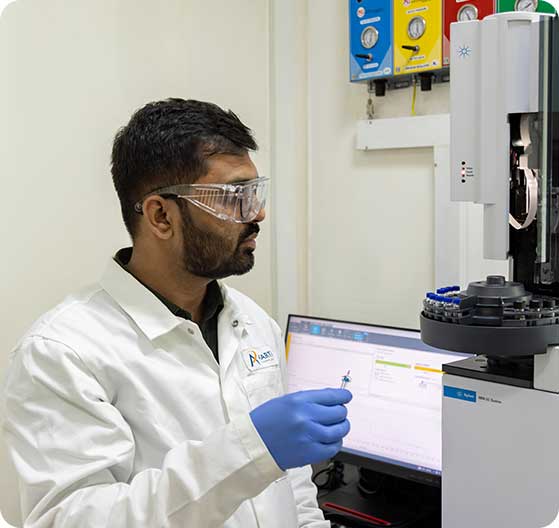
Conduct Proven Acceptable Range (PAR) and Normal Operating Range (NOR) studies to establish robust operating conditions and support regulatory filings.
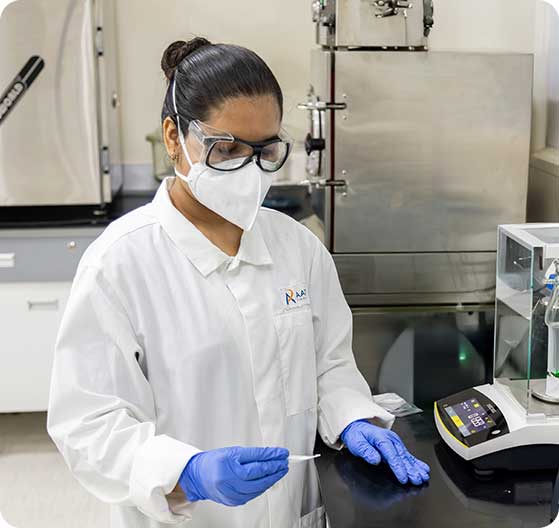
Generate stability data, perform stress testing, and evaluate process safety using RC1mx, DSC, and TSU studies for both powder and liquid systems.
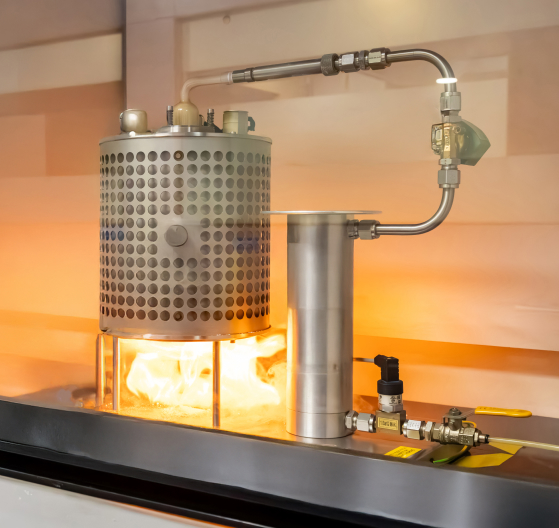
Seamlessly transfer optimized processes and associated knowledge to internal manufacturing plants for scale-up and commercial production.
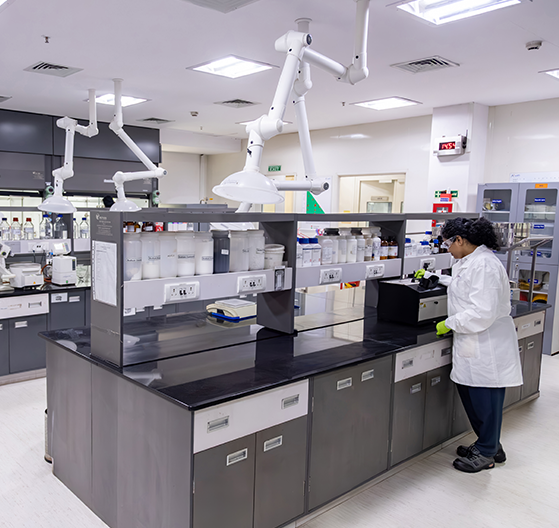
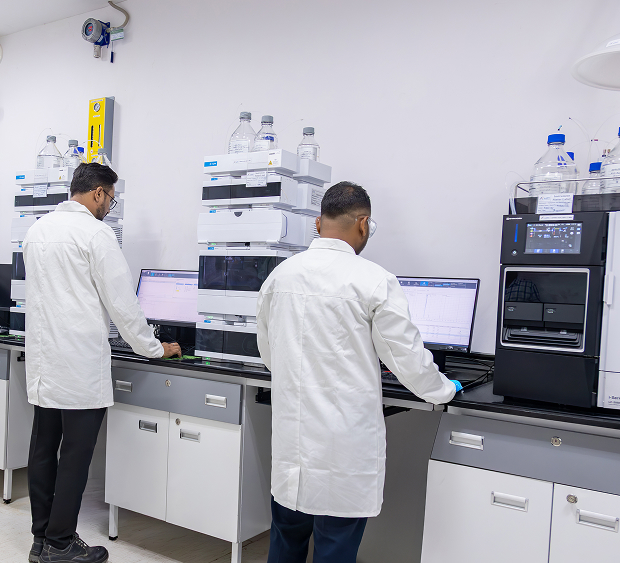
With expertise in analytical method development and advanced analytical instrumentation, we provide comprehensive analytical solutions to support NCE and API development across the product lifecycle.
Safety is embedded throughout our process development lifecycle. Our dedicated Process Safety team evaluates chemical and thermal hazards to identify risks early, optimize process conditions, and enable safe scale-up from laboratory to commercial manufacturing.
Systematic HAZOP studies and risk assessments to identify process hazards, evaluate risks, and establish effective control measures.
Comprehensive evaluation of reaction and thermal hazards using advanced calorimetric techniques to understand heat generation, accumulation, and decomposition risks.
Advanced studies for both liquid and powder systems to assess reaction behavior, thermal stability, dust explosion risks, and safe operating conditions.
Our Process and Powder Safety laboratory is equipped with RC1mx, TSU, DSC, Minimum Ignition Energy Test (MIE), Minimum Ignition Temp. Test (MIT), Layer Ignition Temp. Test (LIT), Ball Fall Hammer, capabilities for in-depth process safety evaluation.
Generating critical safety data to define safe operating parameters, support process optimization, and enable reliable scale-up to commercial manufacturing.
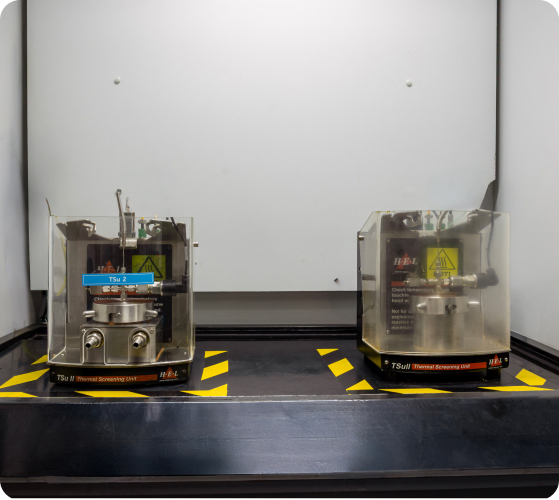
From process understanding to commercial scale, our process safety studies help build safer, more robust, and scalable manufacturing processes.
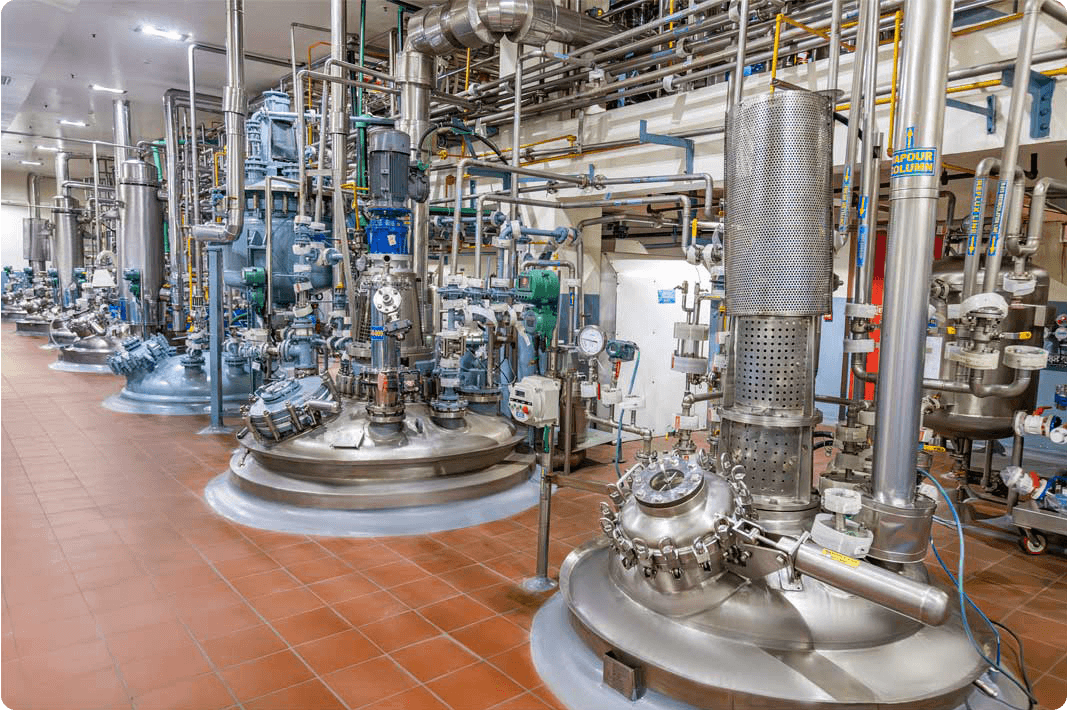
Our integrated capabilities enable robust process validation and reliable production of APIs and intermediates, with a strong focus on quality, consistency, safety, and scalability.
Our experienced technical and manufacturing teams develop and execute robust process validation strategies to demonstrate that manufacturing processes consistently deliver products meeting predefined quality and performance requirements.
 Process validation and PPQ support Process performance monitoring Critical process parameter and critical quality attribute evaluation Scale-up and process optimization Continued process verification Technology transfer and manufacturing readiness
Our commercial manufacturing capabilities enable the reliable production of APIs, intermediates, and complex molecules from development through large-scale production. With scalable infrastructure, experienced operations teams, and robust quality systems, we deliver consistent manufacturing performance across batch sizes.
We focus on operational excellence, supply reliability, process robustness, and on-time delivery, helping customers transition confidently from clinical development to commercial supply.
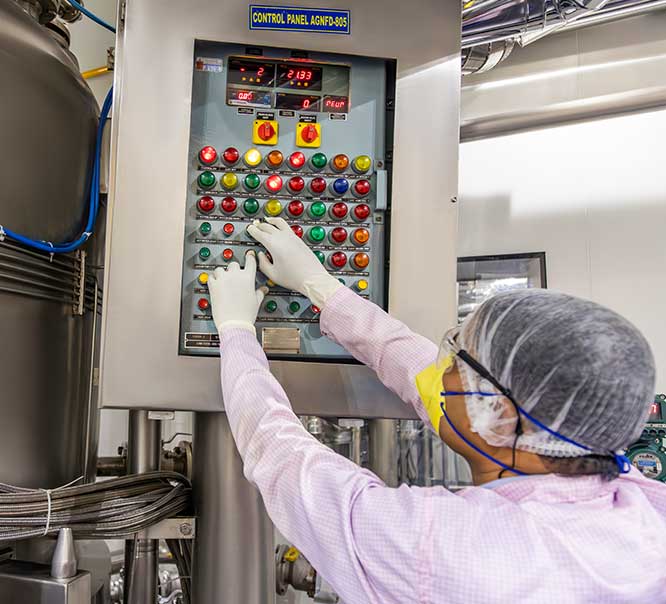
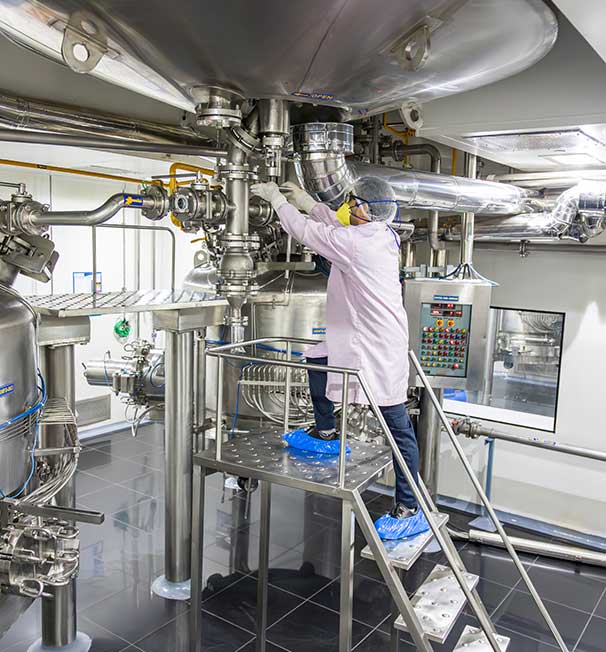
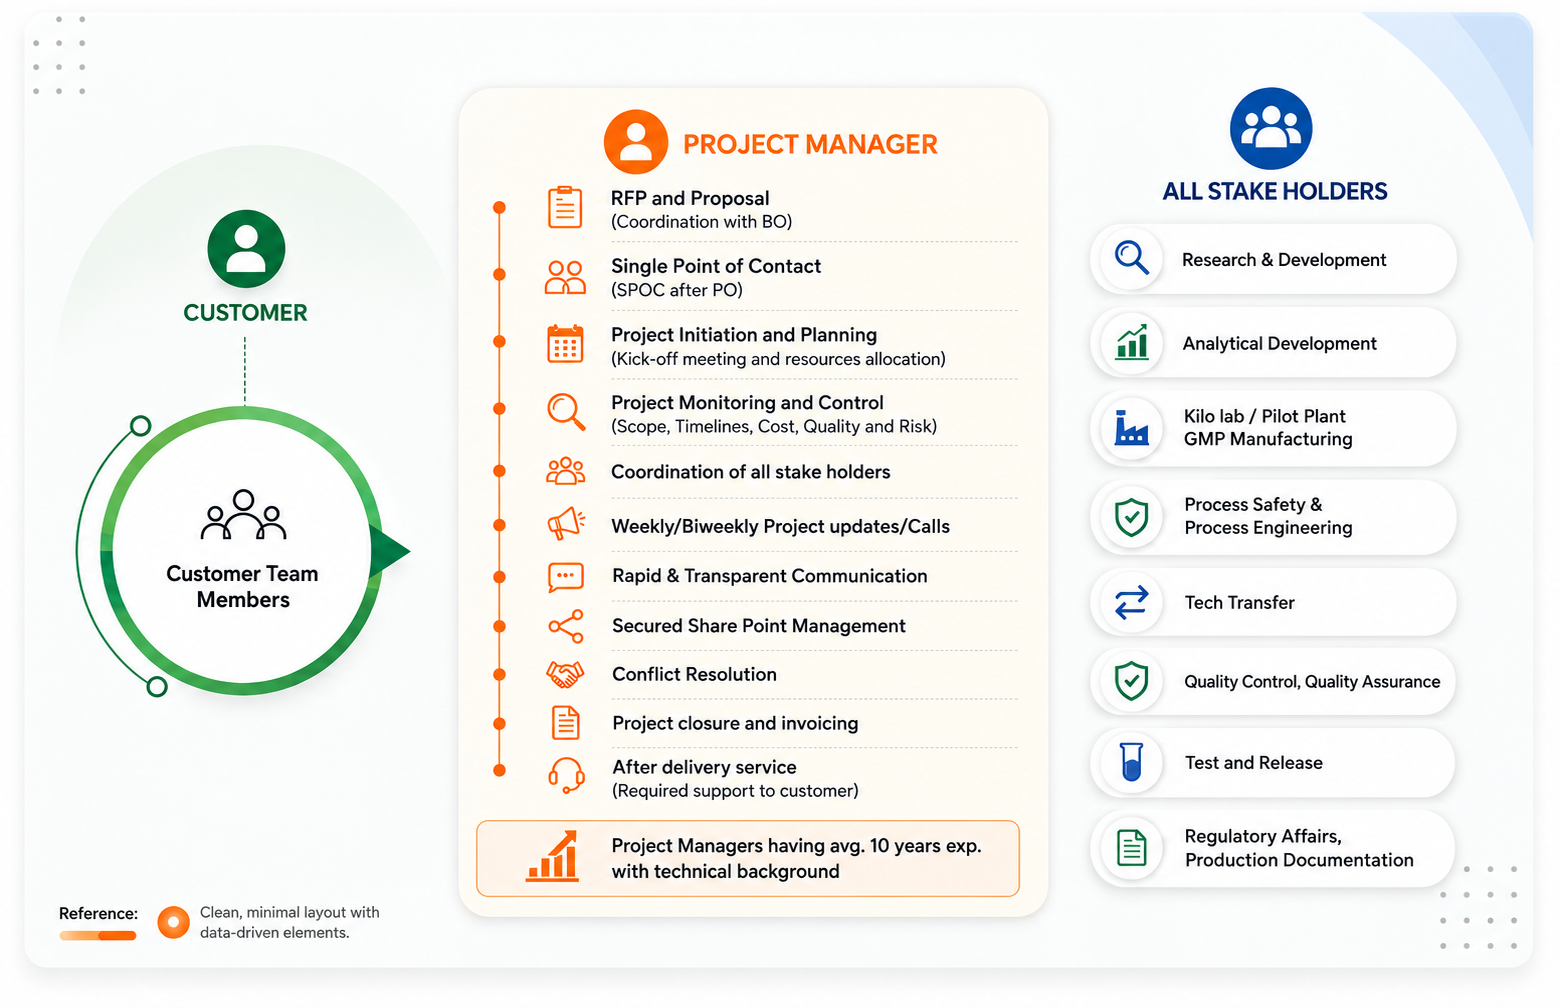
When your CMC program stays with APL, the benefits compound at every stage. Our integrated approach ensures continuity from early development through commercial manufacturing:
At Aarti Pharmalabs Limited (APL), we recognise that intellectual property, confidential information and proprietary know-how are critical to our clients’ success. We are committed to protecting customer information and project-related intellectual property through a people-oriented, legally compliant and robust information security framework.
We continuously strengthen employee awareness and accountability through:
Intellectual property and confidential information generated or shared during customer projects are protected in accordance with contractual confidentiality obligations, applicable laws as per the signed agreements.
Our information security framework (ISO/IEC 27001 Certification) is designed to protect customer data and confidential project information throughout its lifecycle.
We maintain appropriate controls to ensure that confidential information is accessible only to authorised personnel and is handled securely throughout the project lifecycle.
Your intellectual property is entrusted to us. We are committed to protecting it with the same care and responsibility with which we protect our own.
For any questions regarding our intellectual property, confidentiality or information security practices, please contact us.