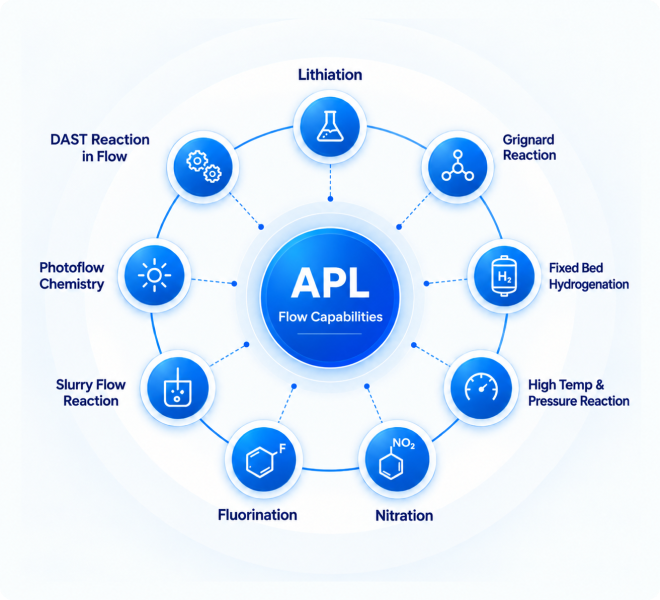
Our flow chemistry platform enables the development and scale-up of efficient, safe, and scalable continuous processes – from laboratory proof-of-concept through commercial manufacturing. Integrated with our process development capabilities, flow chemistry allows us to optimize reaction conditions, improve process control, and accelerate scale-up while maintaining consistent product quality.
Our flow chemistry capabilities are co-located with process development and supporting analytical infrastructure, enabling close collaboration between chemistry, engineering, analytical, and manufacturing teams. This integrated approach supports rapid transition from proof-of-concept to process optimization, scale-up, and commercial production.
Upcoming Flow Technologies
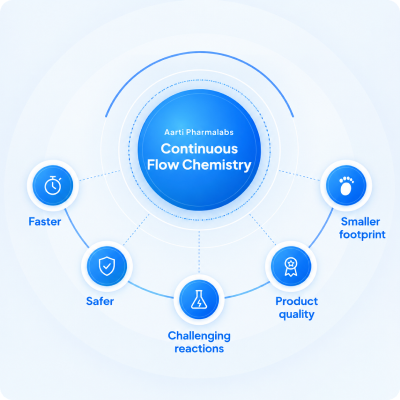
Rapid experimentation and screening of critical parameters accelerate process understanding and reduce development timelines.
Enables higher reaction productivity and reduced reactor volumes, creating more efficient and compact manufacturing processes.
Facilitates translation from laboratory development to larger-scale continuous production while maintaining consistent process performance.
Enables precise control of temperature, residence time, mixing, and reaction conditions, reducing risks associated with hazardous, highly exothermic, or unstable reactions.
Improved heat and mass transfer can deliver better conversion, selectivity, impurity control, and process consistency.
Optimized continuous processing can reduce solvent, reagent, and energy requirements, supporting more sustainable manufacturing.
Creates opportunities to safely and efficiently develop reactions that may be difficult to perform using conventional batch processing.
Flow reactions can be integrated with complementary continuous unit operations, enabling streamlined and scalable end-to-end processes.
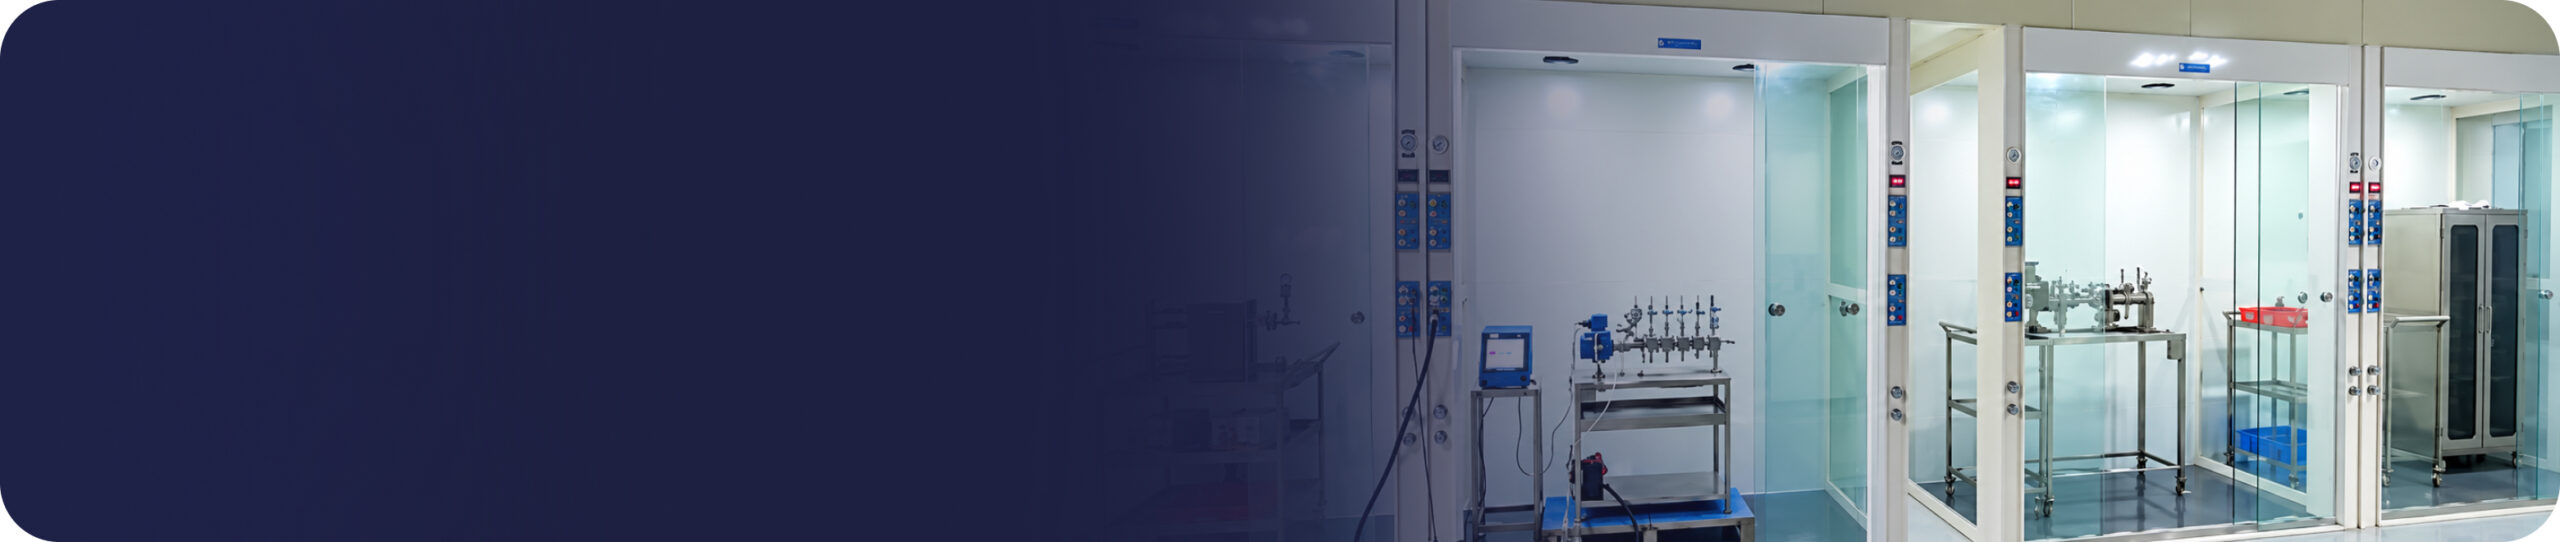

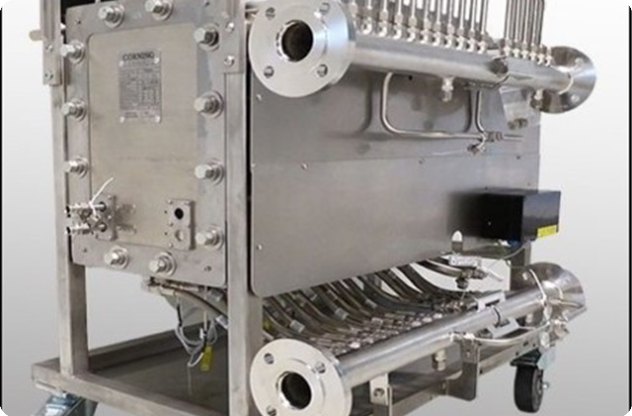 Corning G5 Reactor
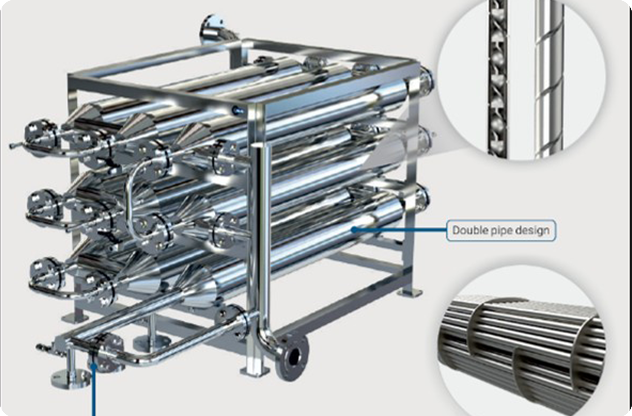 CorFlo Reactor – 5L (HC-276)
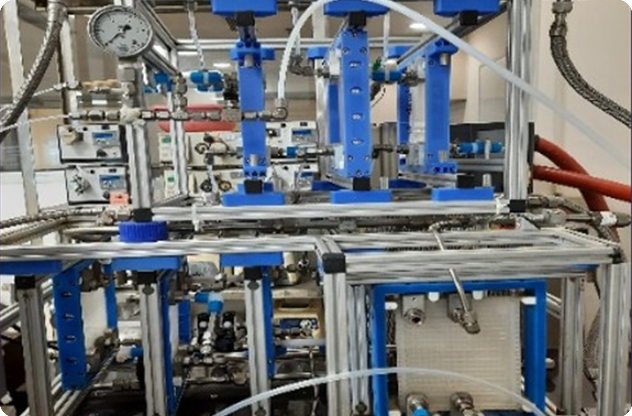 Corning G1 Reactor
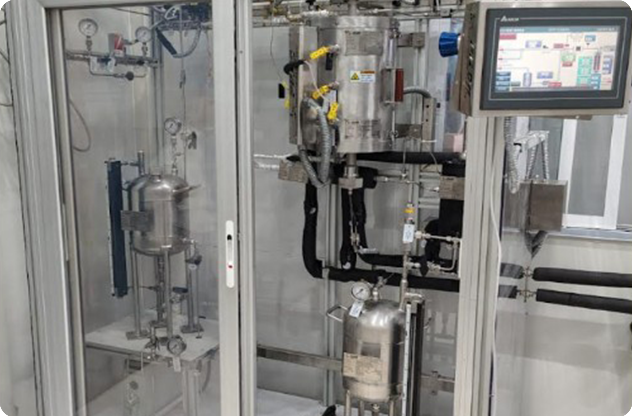 Fixed Bed Reactor
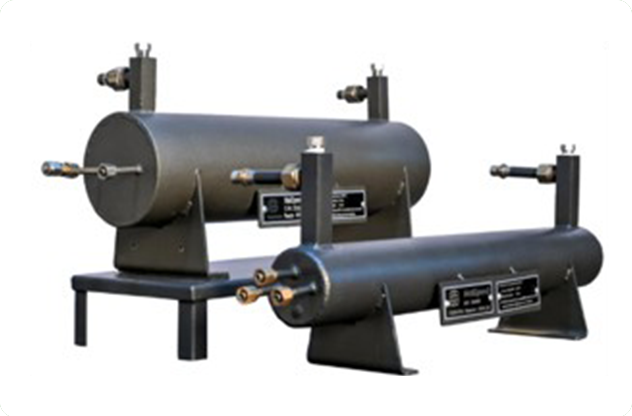 MakSpeed Intenseflo Reactor (HC-276)
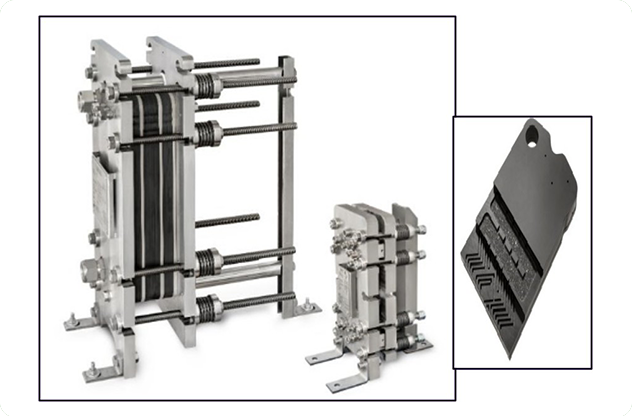 Plantrix® MR260 (SiC_ 32 mL)
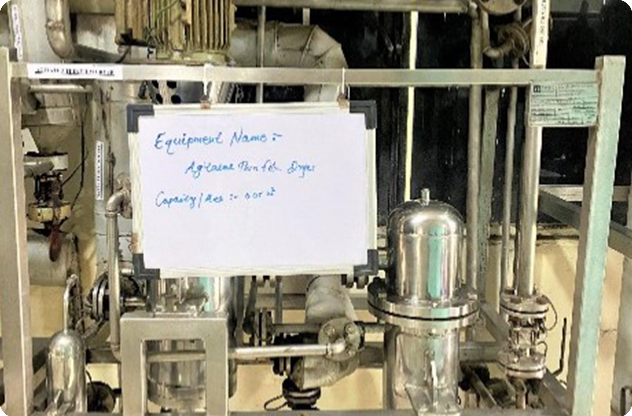 Agitated Thin Film Dryer
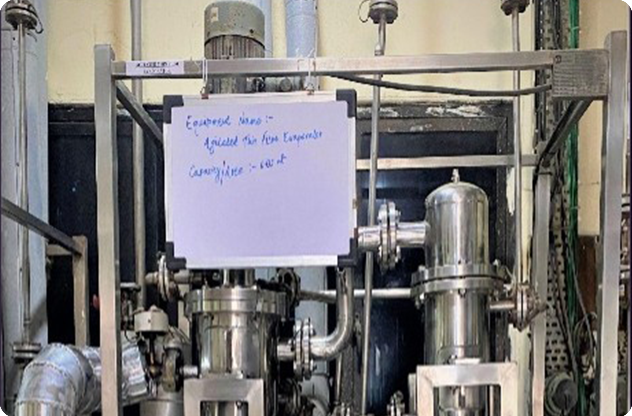 Agitated Thin Film Evaporator
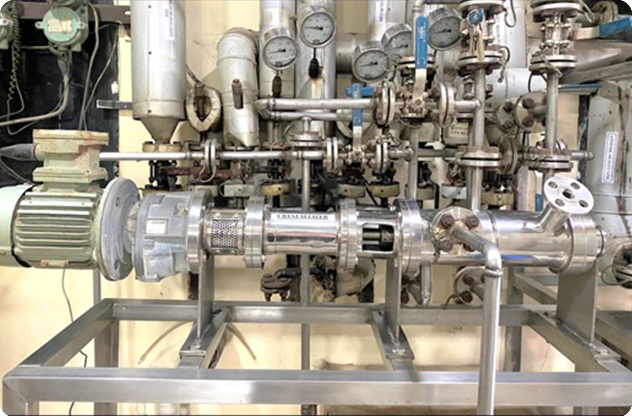 Continuous Crystallizer
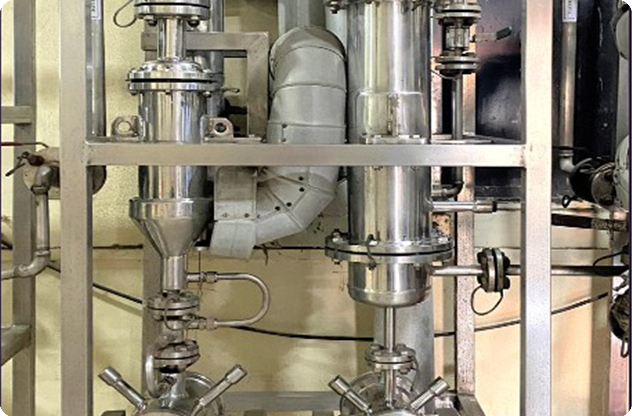 Falling Film Evaporator (FFE)
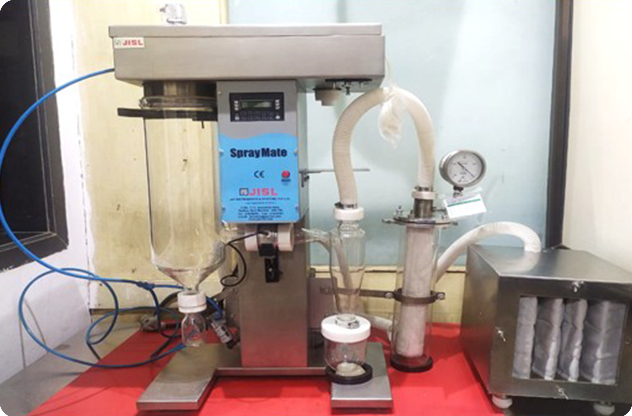 Spray Dryer